Troubleshooting Common Indicator Light Issues

Introduction

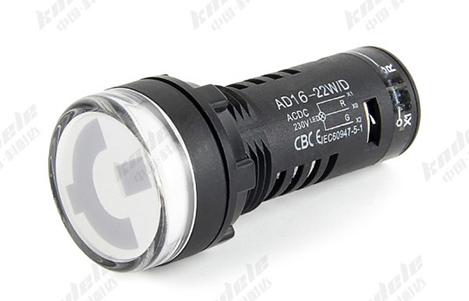
Indicator lights are essential components in industrial, commercial, and automation systems. They provide operators with real-time information about equipment status, helping prevent faults, accidents, and downtime. However, like any electrical device, indicator lights can experience issues that affect visibility, accuracy, or reliability. Understanding how to troubleshoot these problems is key to maintaining efficient and safe operations.
Common Problems with Indicator Lights

Indicator Light Not Turning On

Possible Causes:

Power supply issues (no voltage or blown fuse)

Loose or disconnected wiring

Burned-out LED or bulb

Incorrect voltage rating

Troubleshooting Steps:

Verify the power supply to the light. Check fuses, circuit breakers, and connections.

Inspect wiring for loose or damaged connections.

Confirm that the indicator light matches the system voltage.

Replace the light if it is burned out or defective.

Flickering or Intermittent Operation

Possible Causes:

Loose connections or poor soldering

Voltage fluctuations in the system

Aging or low-quality LED components

Troubleshooting Steps:

Check and tighten all electrical connections.

Measure the system voltage to ensure it is stable and within the indicator’s range.

Replace aging or low-quality indicators with industrial-grade LEDs.

Dim or Weak Light

Possible Causes:

Low input voltage

Dirty or obstructed lens

Aging LED or incandescent bulb

Troubleshooting Steps:

Verify that the voltage supplied to the indicator is correct.

Clean the lens or cover to remove dust or grime.

Replace the indicator if the light output is insufficient due to aging.

Wrong Color or Confusing Signals

Possible Causes:

Incorrect wiring or cross-connection

Faulty bi-color or tri-color indicator

Lack of standard color coding

Troubleshooting Steps:

Double-check wiring according to the schematic.

Test the indicator function individually to ensure correct color transitions.

Implement standard color coding (green = normal, red = fault, yellow = warning).

Excessive Heat or Burned Indicator

Possible Causes:

Over-voltage or incorrect current rating

Prolonged operation beyond design limits

Poor ventilation in enclosed panels

Troubleshooting Steps:

Confirm that the indicator light is rated for system voltage and current.

Ensure proper ventilation around the panel or mounting area.

Replace the indicator if it is damaged by overheating.

Tips for Preventing Indicator Light Issues

Use High-Quality Components – Invest in industrial-grade LEDs for reliability.

Follow Wiring Standards – Correct installation reduces wiring errors and signal confusion.

Regular Maintenance – Inspect indicators during routine checks and clean lenses.

Monitor Environmental Conditions – Protect lights from excessive heat, moisture, or dust.

Integrate with Smart Systems – Remote monitoring can alert operators to early signs of indicator failure.

Conclusion

Troubleshooting indicator light issues is crucial for maintaining safe and efficient industrial operations. By identifying common problems such as non-functioning lights, flickering, dimming, wrong colors, or overheating, operators can take timely action to prevent equipment downtime and improve safety.

Proper installation, maintenance, and selection of high-quality indicators ensure long-lasting performance, reducing the need for frequent replacements and supporting smooth workflow in industrial, commercial, and automation systems.

FAQ

Q1: How can I tell if an LED indicator is faulty?
A: Check if the light fails to turn on, flickers, or shows inconsistent colors despite correct wiring and voltage.

Q2: Can flickering indicators damage equipment?
A: Usually, they do not harm equipment, but they indicate unstable voltage or loose connections that should be corrected.

Q3: How often should indicator lights be inspected?
A: Ideally, during routine maintenance cycles, such as monthly or quarterly inspections, depending on system criticality.
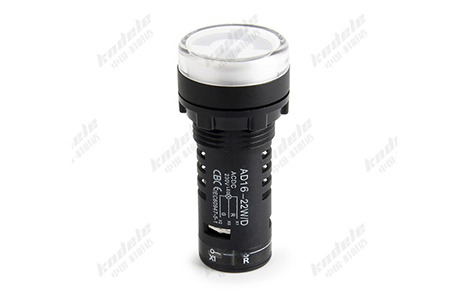
LED Indicator Lights: Energy Efficiency and Longevity Advantages

Introduction

In modern industrial and electrical systems, LED indicator lights have become the standard choice for signaling and monitoring. Compared to traditional incandescent or neon indicators, LEDs offer significant advantages in energy efficiency, lifespan, and overall reliability. This article explores why LED indicator lights are preferred in industrial, commercial, and automation applications.

What Are LED Indicator Lights?

LED (Light Emitting Diode) indicator lights are electronic devices that emit light when an electrical current passes through a semiconductor. Unlike traditional bulbs, LEDs do not rely on filaments or gas discharge, which makes them more durable, energy-efficient, and long-lasting.

Key Characteristics:

Compact and lightweight design

Low energy consumption

High brightness and visibility

Fast response and instant-on operation

Available in multiple colors for status signaling

Energy Efficiency of LED Indicator Lights

One of the most notable advantages of LED indicator lights is their energy efficiency:

Low Power Consumption
LED indicators consume significantly less electricity than incandescent or neon lights. This not only reduces energy costs but also minimizes heat generation on control panels.

Sustainable Choice
Reduced energy consumption translates to a smaller carbon footprint, making LEDs a greener option for factories, commercial buildings, and smart industrial systems.

Ideal for Large Installations
In industrial facilities with dozens or hundreds of indicator lights, switching to LEDs can result in substantial energy savings over time.

Longevity and Durability

LED indicator lights are built to last, providing long-term reliability for industrial applications:

Extended Lifespan
LED indicators can last 50,000 hours or more, compared to 1,000–5,000 hours for incandescent bulbs. This reduces the frequency of replacements and maintenance costs.

Resistance to Shock and Vibration
Unlike filament bulbs, LEDs are solid-state devices that can withstand vibrations and mechanical shocks, which is crucial in industrial environments.

Performance in Extreme Conditions
High-quality LED indicators function reliably under a wide range of temperatures and environmental conditions, including humidity, dust, and chemical exposure.

Applications of LED Indicator Lights

LED indicator lights are widely used in industrial, commercial, and automation systems due to their reliability and visibility:

Control Panels – Display equipment status, power-on, fault, or warning signals

Industrial Machines – Monitor operational states and guide maintenance

Automation and Robotics – Provide quick visual feedback in PLC and IoT-controlled systems

Energy Management Systems – Indicate power usage or system alerts in smart buildings

Electrical Switchgear – Ensure clear signaling in low- and medium-voltage circuits

Advantages Over Traditional Indicator Lights

Feature LED Indicator Lights Incandescent/Neon Lights
Energy Consumption Very low High
Lifespan 50,000+ hours 1,000–5,000 hours
Durability Resistant to shock/vibration Fragile
Heat Generation Minimal Significant
Color Variety Wide range Limited

The combination of energy savings, durability, and high visibility makes LEDs the preferred choice for modern industrial and automation systems.

Best Practices for Using LED Indicator Lights

Choose the Right Color – Use standard color codes (green = normal, red = fault, yellow = warning).

Check Voltage Compatibility – Ensure LED indicators match the system voltage and current requirements.

Install in Visible Locations – Maximize visibility for operators and maintenance personnel.

Integrate with Smart Systems – Connect LEDs to PLCs, SCADA, or IoT devices for remote monitoring and predictive maintenance.

Conclusion

LED indicator lights have revolutionized industrial signaling by combining energy efficiency, long lifespan, and durability. Their low power consumption, high reliability, and wide range of applications make them ideal for modern control panels, automation systems, and industrial equipment.

Investing in LED indicators not only improves operational efficiency but also reduces maintenance costs and supports sustainable, energy-conscious operations.

FAQ

Q1: Can LED indicator lights replace traditional neon lights in high-voltage systems?
A: Yes, as long as the LED indicators are rated for the system voltage and designed for industrial use.

Q2: How much energy can an LED indicator save?
A: An LED indicator can consume up to 90% less power than an incandescent bulb, which adds up significantly in large-scale installations.

Q3: Are LED indicator lights suitable for harsh industrial environments?
A: Yes, they are resistant to shock, vibration, temperature extremes, and other challenging conditions.

Types of Indicator Lights and Their Applications

Introduction

In industrial and electrical systems, indicator lights are crucial for conveying the status of machinery, circuits, and processes. Choosing the right type of indicator light ensures efficient monitoring, safety, and smooth operation of industrial equipment. This article explores the main types of indicator lights and their typical applications in industrial and commercial settings.

LED Indicator Lights

LED (Light Emitting Diode) indicator lights are the most popular choice in modern industrial applications due to their efficiency, longevity, and brightness.

Key Features:

Energy-efficient and low power consumption

Long lifespan (often 50,000+ hours)

Fast response time and high visibility

Available in multiple colors for different status signals

Common Applications:

Control Panels: Display machine status such as power-on, fault, or warning

Automation Equipment: Integrated with PLCs for process monitoring

IoT Systems: Provide remote visual feedback in smart factories

Neon Indicator Lights

Neon indicator lights are known for their durability in high-voltage environments and simple design.

Key Features:

Can handle high voltage applications

Simple, robust, and reliable

Low maintenance

Common Applications:

High-Voltage Switchgear: Indicating circuit status in substations

Legacy Industrial Equipment: Used in older machines and panels

Power Supply Units: Signaling presence of AC power

Incandescent Indicator Lights

Incandescent lights are traditional indicator lights that have been used for decades. Though less energy-efficient than LEDs, they are still found in certain applications.

Key Features:

Warm light, easily visible

Simple technology, low initial cost

Shorter lifespan compared to LEDs

Common Applications:

Legacy Panels and Equipment: Retrofitting old control systems

Low-Cost Industrial Devices: Where replacement cost is a concern

Visual Feedback in Low-Intensity Environments

Bi-Color and Tri-Color Indicator Lights

Bi-color and tri-color lights can display multiple statuses using a single indicator by switching or mixing colors.

Key Features:

Reduce the number of indicators needed on a panel

Show multiple machine states, e.g., standby, running, fault

Available in LED or incandescent versions

Common Applications:

Complex Control Panels: Convey multiple system states efficiently

Machinery with Limited Panel Space: Reduce clutter while maintaining clarity

Process Monitoring Systems: Visualizing multi-stage processes

Panel-Mount and PCB-Mount Indicator Lights

Depending on installation requirements, indicator lights can be panel-mounted or PCB-mounted.

Panel-Mount Indicators:

Installed directly on control panels

Provide high visibility and easy access for operators

PCB-Mount Indicators:

Mounted directly on circuit boards

Compact design for electronic equipment and control modules

Common Applications:

Industrial Control Panels: Panel-mounted for machine status visibility

Consumer Electronics & Industrial PCBs: PCB-mounted for compact, efficient design

Selecting the Right Indicator Light

When choosing an indicator light for your application, consider the following factors:

Voltage and Current Rating – Ensure compatibility with your system

Color Coding – Use standard colors (green = normal, red = fault, yellow = warning)

Environmental Conditions – Temperature, moisture, dust, or vibration resistance

Installation Type – Panel-mounted vs PCB-mounted, visible from intended angles

Integration Needs – Compatibility with PLCs, SCADA, or IoT systems

Conclusion

Understanding the types of indicator lights and their applications is essential for designing reliable and safe industrial systems. From energy-efficient LEDs to high-voltage neon lights, each type has specific advantages depending on the operating environment and system requirements. Proper selection and installation of indicator lights not only improve system monitoring and safety but also streamline maintenance and operational efficiency.

Whether upgrading legacy equipment or building a modern smart factory, choosing the right indicator light ensures clarity, reliability, and efficiency across your industrial systems.

FAQ

Q1: What is the difference between LED and neon indicator lights?
A: LEDs are energy-efficient, long-lasting, and suitable for low-voltage systems, while neon lights are robust and ideal for high-voltage applications.

Q2: Can a single bi-color indicator replace multiple single-color lights?
A: Yes, bi-color and tri-color indicators can display multiple machine states using one device, saving panel space.

Q3: Are PCB-mounted indicator lights suitable for industrial environments?
A: Yes, but they are best for enclosed equipment or control modules where the indicator is visible, rather than open industrial panels.

Understanding Indicator Lights: Function and Importance in Industrial Systems

Introduction

In modern industrial environments, keeping machines and processes running smoothly requires constant monitoring and quick response to issues. One of the most fundamental yet often overlooked components in industrial systems is the indicator light. These small, seemingly simple devices play a critical role in ensuring safety, efficiency, and reliability in factories, control panels, and electrical systems.

What Is an Indicator Light?

An indicator light is a visual signaling device that conveys the operational status of machinery or electrical circuits. Typically installed on control panels, machinery, or equipment, these lights can:

Show whether a machine is powered on or off

Indicate operating conditions or faults

Alert operators to maintenance requirements or safety issues

They come in various types, such as LED, incandescent, and neon lights, and are designed for specific voltages, currents, and industrial environments.

Functions of Indicator Lights in Industrial Systems

Operational Status Monitoring
Indicator lights provide immediate visual feedback about equipment status. For example, a green light might signal normal operation, while a red light warns of a fault. This allows operators to respond quickly without stopping production unnecessarily.

Safety and Hazard Prevention
In industrial settings, safety is paramount. Indicator lights alert personnel to dangerous conditions such as overheating, short circuits, or emergency shutdowns. This proactive warning helps reduce workplace accidents and equipment damage.

Maintenance and Diagnostics
Indicator lights often guide maintenance schedules. For example, a blinking yellow light might indicate that a filter needs replacement or that a system requires inspection. This reduces downtime and improves preventive maintenance practices.

System Efficiency and Workflow Optimization
By clearly showing the operational state of equipment, indicator lights allow operators to manage workflow efficiently. Quick visual cues reduce the need for manual checking and speed up troubleshooting.

Types of Indicator Lights Commonly Used

LED Indicator Lights: Energy-efficient, long-lasting, and ideal for high-frequency signaling.

Neon Indicator Lights: Durable in high-voltage applications but less energy-efficient.

Incandescent Indicator Lights: Traditional type, often used in legacy equipment, but with shorter lifespan.

Each type has its advantages depending on the application, voltage rating, and environmental conditions such as temperature, humidity, or exposure to dust and chemicals.

Why Indicator Lights Are Essential in Industrial Systems

Enhance Safety Compliance
Industrial standards often require visual indicators to signal emergency or abnormal conditions. Indicator lights help companies comply with occupational safety regulations.

Reduce Downtime
Quick identification of faults or abnormal conditions minimizes production delays and prevents costly shutdowns.

Improve Operator Efficiency
With clear, easily interpretable signals, operators can make faster, more accurate decisions.

Support Automation and Smart Monitoring
Modern indicator lights integrate with PLCs, SCADA systems, and IoT networks, allowing remote monitoring and predictive maintenance.

Best Practices for Using Indicator Lights

Choose the Right Color Coding: Standardize green for normal operation, red for faults, yellow for warnings, and blue for auxiliary signals.

Ensure Visibility: Place indicator lights where they can be easily seen by operators, considering angles and distances.

Match Voltage and Environment: Select lights rated for the operating voltage and suitable for harsh industrial environments.

Integrate with Automation Systems: Connect indicator lights to PLCs or remote monitoring systems for real-time alerts.

Conclusion

While small and simple, indicator lights are vital components in industrial systems. They provide real-time status information, enhance safety, support maintenance, and improve workflow efficiency. Whether in legacy machinery or modern automated plants, properly selected and installed indicator lights ensure smooth, safe, and efficient operations.

For industrial automation and electrical equipment suppliers, offering high-quality indicator lights not only improves system reliability but also builds trust with clients who rely on consistent performance and safety.

FAQ

Q1: Can LED indicator lights be used in high-voltage industrial systems?
A: Yes, as long as they are rated for the voltage and environmental conditions of the system.

Q2: How do indicator lights differ from warning buzzers or alarms?
A: Indicator lights provide visual signals, while buzzers or alarms provide audible alerts. Often, both are combined for maximum safety.

Q3: Are indicator lights compatible with IoT and smart factory systems?
A: Modern LED indicator lights can integrate with PLCs, SCADA, and IoT networks for remote monitoring and predictive maintenance.