

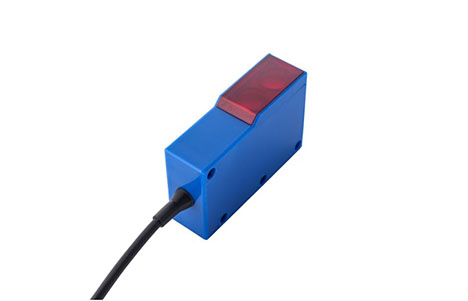
Photoelectric switches, also known as photoelectric sensors, have become a cornerstone in modern industrial automation. By detecting objects or changes in their environment using light, they enable precise, fast, and non-contact detection. From manufacturing lines to packaging systems, photoelectric switches improve efficiency, safety, and reliability across multiple industries. In this blog, we will explore the top applications of photoelectric switches in industrial automation.
 Conveyor Belt Object Detection
One of the most common applications of photoelectric switches is object detection on conveyor belts. These sensors can:
Detect the presence or absence of products
Trigger downstream equipment like sorters, diverters, or packaging machines
Count items accurately without physical contact
Example: In a food processing plant, photoelectric switches ensure every item on a conveyor is properly detected before packaging, preventing misplacement or jams.
Photoelectric switches are widely used in automated packaging lines to improve speed and accuracy. They can:
Verify product positioning
Detect filled or empty containers
Trigger packaging or labeling equipment
Benefit: By using photoelectric sensors, packaging systems achieve high precision while reducing manual inspection and downtime.
Safety is critical in industrial automation. Photoelectric switches can be integrated into safety barriers to protect operators from machinery hazards.
Infrared beams create invisible “light curtains” around dangerous areas
Machines stop automatically if the beam is interrupted
Ensures compliance with safety standards
Example: Robotic welding stations often use photoelectric safety sensors to prevent accidental operator injuries.
In assembly and manufacturing lines, photoelectric switches are ideal for counting parts or tracking their position.
High-speed counting of small components
Detecting precise alignment for robotic assembly
Triggering downstream operations based on object position
Benefit: This reduces errors and ensures consistent quality in mass production.
Photoelectric switches can detect objects of varying sizes, shapes, or colors, making them perfect for sorting and quality control applications.
Sort defective or misaligned products
Detect missing components on assembly lines
Ensure products meet visual or dimensional standards
Example: Electronics assembly lines use photoelectric sensors to check the presence of chips and connectors before soldering.
In industries such as food, beverage, or chemical processing, photoelectric switches can monitor liquid levels in containers without physical contact.
Detect transparent or opaque liquids
Trigger pumps or alarms automatically
Prevent overflow or underfill
Benefit: Non-contact detection reduces contamination risks and increases reliability.
Photoelectric switches play a crucial role in robotic systems and automated machinery:
Detect objects for robotic picking
Ensure accurate positioning before assembly or processing
Provide feedback for motion control systems
Example: A robotic arm in a warehouse uses photoelectric sensors to identify and pick packages quickly and accurately.
Photoelectric switches are essential components in modern industrial automation, providing fast, accurate, and non-contact detection across a wide range of applications. From conveyor belts and packaging systems to robotics, safety barriers, and quality control, these sensors improve efficiency, reduce downtime, and enhance safety.
By integrating photoelectric switches into your automation systems, industries can achieve higher productivity, better accuracy, and reduced operational risks.
What is a photoelectric switch?
A photoelectric switch (or photoelectric sensor) is a device that detects objects or changes in the environment using a light beam. When the light is interrupted or reflected, the sensor sends an electrical signal.
How are photoelectric switches used in industrial automation?
Photoelectric switches are widely used for:
Detecting objects on conveyor belts
Automated packaging and labeling
Safety barriers and light curtains
Part counting and positioning
Quality control and sorting
Liquid level detection
Robotic pick-and-place systems
What are the main types of photoelectric switches?
Through-beam sensors: Emitter and receiver are separate; the beam is interrupted by objects.
Reflective sensors: Beam reflects off the object back to the sensor.
Retro-reflective sensors: Beam reflects off a reflector and detects interruptions caused by objects.
Can photoelectric switches detect transparent or small objects?
Yes, specially designed photoelectric sensors can detect transparent, opaque, or very small objects, depending on the type of sensor and its sensitivity settings.
What advantages do photoelectric switches offer over mechanical switches?
Non-contact detection, reducing wear and tear
High-speed response, suitable for fast production lines
Accurate detection for counting, sorting, and positioning
Flexible installation in automated systems
Enhanced safety in hazardous areas
Are photoelectric switches suitable for harsh industrial environments?
Yes, but it depends on the sensor type. Many photoelectric switches are IP-rated for dust, moisture, or temperature extremes. Protective housing may be required in very harsh conditions.

